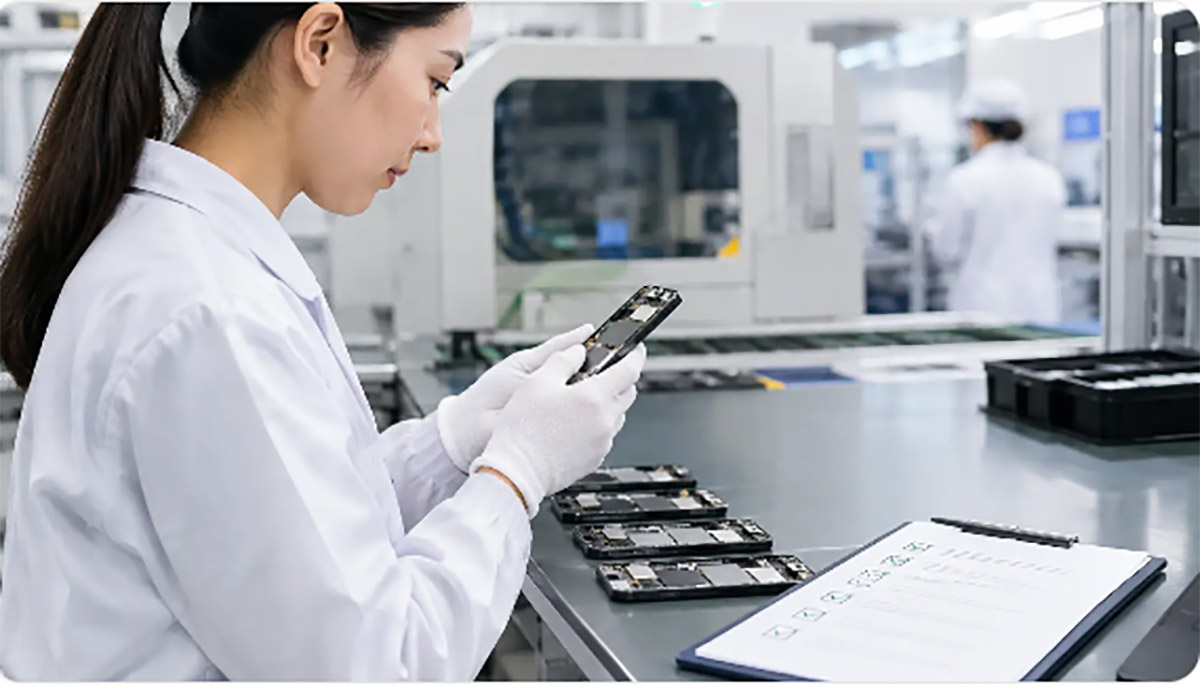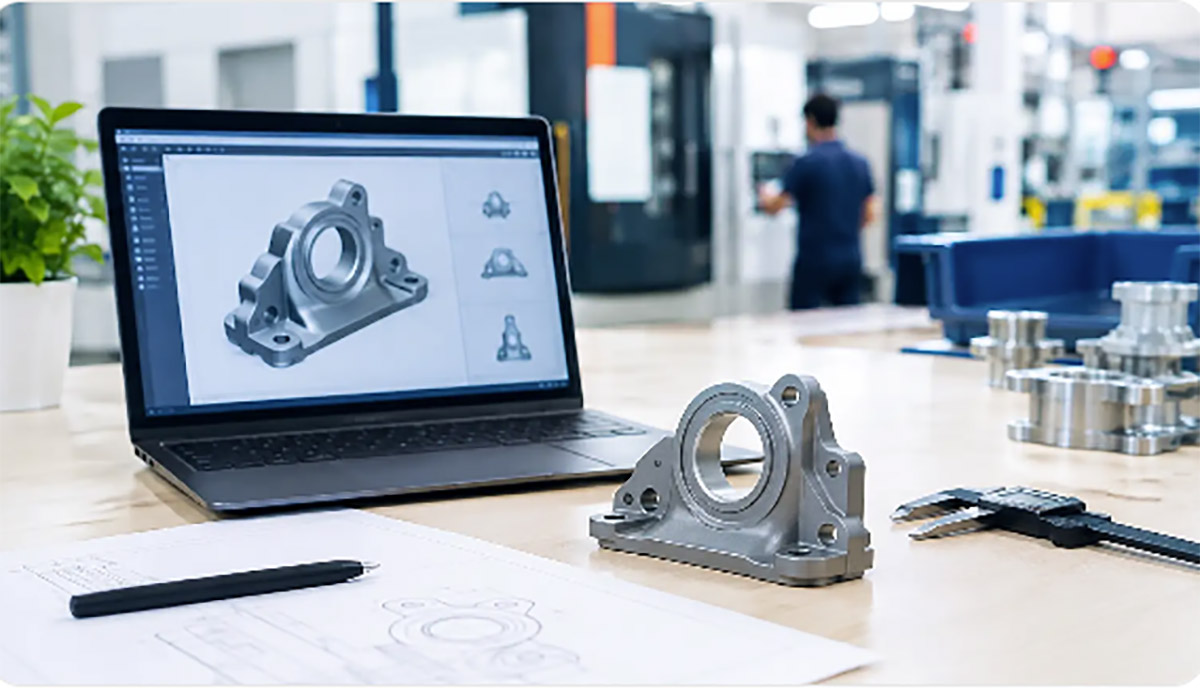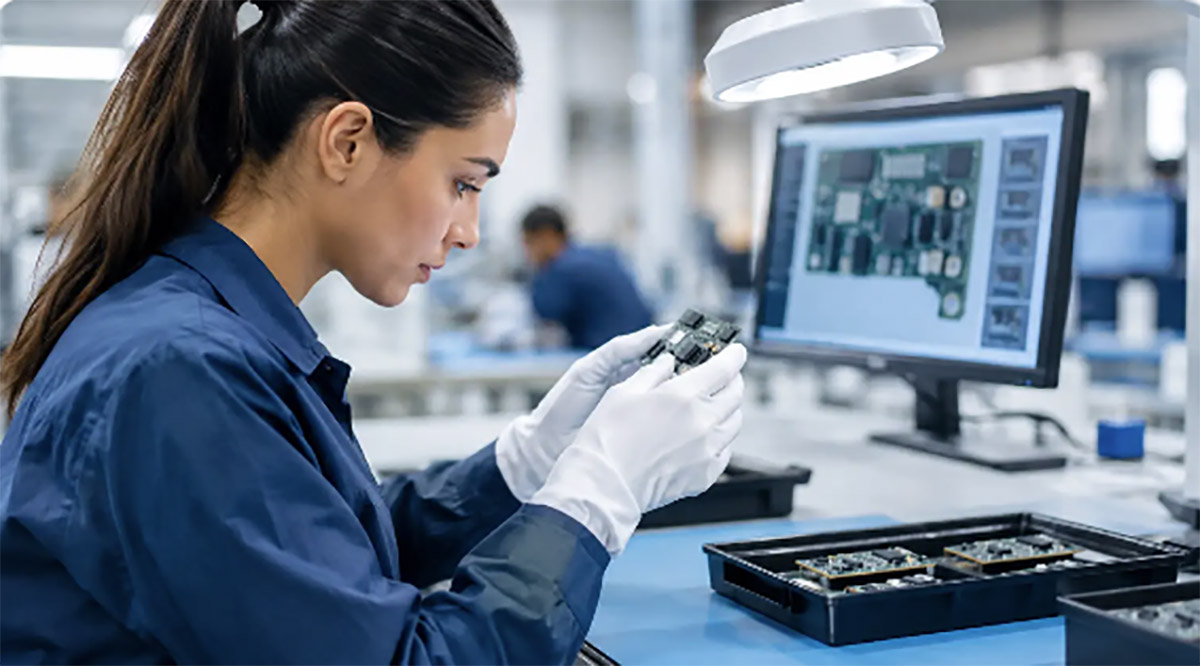
OEM box build assembly brings components, sourcing, testing, and packaging into one controlled production flow for dependable, scalable product delivery.

A product can have well-made
individual parts and still fail at the finish line. The usual causes are not
dramatic: an incorrect cable revision, a missed fastener, firmware loaded to
the wrong version, or packaging that does not protect the unit in
transit. OEM box build assembly addresses these risks by
bringing the complete product build under a controlled manufacturing process
rather than treating final assembly as an afterthought.
For OEM brands, product
companies, and hardware teams, box build is where component quality,
documentation, labor instructions, testing, and delivery requirements meet. A
capable manufacturing partner coordinates those inputs into repeatable finished
goods that are ready for sale, installation, or distribution.
What OEM Box Build Assembly
Includes
OEM box build assembly is the production of a complete
finished product from individual mechanical, electrical, and purchased
components. Depending on the product, the scope can range from installing a few
molded parts and a PCB to building, configuring, testing, labeling, and
packaging a multi-component electronic system.
The term "box build"
is common in electronics manufacturing, but the process applies more broadly.
Consumer devices, industrial controls, smart home products, appliances,
battery-powered tools, medical accessories, and electromechanical assemblies
can all require box build services.
A typical scope may include
component sourcing, incoming inspection, subassembly production, mechanical
assembly, PCB installation, cable and harness routing, firmware programming,
functional testing, cosmetic inspection, serial number control, labeling, and
retail or bulk packaging. The right scope depends on where the customer wants
responsibility to begin and end.
For example, a company may
supply its own PCB assemblies but require the manufacturer to source
injection-molded housings, silicone seals, screws, displays, chargers, and
packaging. Another may need a single supplier to manage every production
component from approved bills of materials through final shipment.
Why Final Assembly Needs Production
Engineering
Final assembly appears straightforward on a product
rendering. On the factory floor, it is a sequence of decisions that can affect
yield, labor cost, product reliability, and delivery dates.
A design may call for a cable
that must pass through a narrow housing feature before a connector is
installed. A screw may require a specified torque to avoid stripping plastic
bosses or creating a loose joint. A gasket may look correctly seated while
still failing an ingress check. These are manufacturing details, not just
assembly tasks.
Before volume production, the
assembly process should be reviewed for design for assembly, or DFA. This review
identifies parts that are difficult to orient, features that require excessive
force, ambiguous fastener locations, and steps that create opportunities for
operator error. It also determines whether fixtures, torque tools, go/no-go
gauges, or test jigs are needed.
A good build process
translates engineering intent into controlled work instructions. Those
instructions should define the assembly sequence, approved materials, tool
settings, inspection points, acceptance criteria, and traceability
requirements. Photos, diagrams, and reference samples are often necessary for
products with cosmetic or orientation-sensitive features.
The Cost of Skipping Process
Development
Without a defined process, operators may build the
same unit in different ways. That variation increases rework and makes
root-cause analysis difficult when field failures occur. It can also conceal a
design issue until a production run is already underway.
Process development adds work
before production, but it is usually less expensive than sorting finished
inventory, replacing products in the field, or stopping a launch because one
sourced part does not fit. The needed level of preparation depends on volume
and product complexity. A low-volume industrial unit may justify more manual
inspection, while a consumer product built at scale may require dedicated
fixtures to maintain cycle time and consistency.
Building the Supply Chain Around
the Finished Product
Box build performance depends on more than the
assembly line. Every component needs an approved specification, revision
control, and a practical sourcing plan.
Mechanical parts can include
injection-molded housings, die-cast frames, stamped brackets, machined
components, silicone keypads, adhesive pads, and custom fasteners. Electronic
content may include PCB assemblies, batteries, displays, sensors, connectors,
antennas, power supplies, and cable harnesses. Packaging introduces another set
of production materials, such as cartons, trays, inserts, labels, manuals, and
protective bags.
Managing these parts through
multiple suppliers creates coordination risk. A late display, an out-of-spec
molded cover, or a revised printed manual can hold up final shipment even when
most of the product is complete. Integrated sourcing helps reduce these gaps
because procurement, quality, and assembly planning can work from the same
production schedule and bill of materials.
That does not mean every
component should automatically be sourced from one factory. Customers may
retain control of proprietary electronics, nominated components, or strategic
suppliers. The practical goal is clear ownership: each item should have an
approved source, revision status, lead time, incoming inspection standard, and
replacement path if supply is disrupted.
Quality Control During OEM Box
Build Assembly
Quality cannot be recovered
through final inspection alone. Final checks can identify defects, but they do
not prevent the same defect from being built into the next unit. Effective quality control places checkpoints at
the stages where problems are most likely to occur.
Incoming inspection confirms
that critical purchased parts match the approved specification. During
assembly, operators and inspectors verify details such as torque values,
connector engagement, adhesive placement, cable routing, and cosmetic fit.
Functional testing confirms that the assembled product performs as intended
before packaging.
For products requiring
traceability, each unit can be linked to a serial number, production batch,
firmware version, test result, and key component lot. This level of control is
especially useful for electronics, regulated applications, warranty programs,
and products with field-service requirements.
Functional test requirements
should be defined early. A basic test may confirm power-up, button response,
LED operation, charging, and communication. More complex products may require
programmed test fixtures, measurement equipment, burn-in periods, or
calibration. The test method should match the product risk. Testing every
possible feature on every unit may be unnecessary for a simple accessory, while
limited testing is not adequate for a safety-critical or high-value device.
Cosmetic Standards Need Clear
Limits
Cosmetic inspection is often underestimated. Color
variation between molded parts, uneven gaps, scratches, sink marks, dust under
a display lens, and label misalignment can all affect customer acceptance even
when the product functions correctly.
The most useful cosmetic
standard is specific. It defines inspection distance, lighting conditions,
visible surfaces, acceptable variation, and reference samples. Terms such as
"good appearance" leave too much room for interpretation. Clear
standards allow the factory and customer to make consistent decisions before
thousands of units are packed.
Packaging Is Part of the Product
Build
Packaging is not only a shipping requirement. It
affects assembly time, presentation, product protection, labeling accuracy, and
fulfillment efficiency.
A finished unit may need
protective film, accessories, manuals, molded trays, charging cables, barcode
labels, master cartons, and pallet configuration. Each item must be checked
against the correct product revision and destination requirement. Retail-ready
packaging may need stricter visual control, while industrial shipments may
prioritize durable bulk packing and easy identification.
Packaging validation should
consider vibration, compression, and handling during normal distribution. A
visually attractive box that allows a product to move inside can create
warranty costs and damaged inventory. Conversely, excessive packaging can
increase material cost, packing labor, freight volume, and environmental
burden.
Choosing the Right Box Build
Partner
The right partner should be evaluated on process
capability, not simply quoted unit price. Ask how the supplier manages BOM
revisions, controls incoming materials, documents work instructions, handles
nonconforming parts, and records test results. Review whether it can produce
the required mechanical components, source electronics, build fixtures, perform
assembly, and manage packaging under coordinated quality oversight.
It is also useful to
understand how the supplier supports the transition from prototype to
production. Prototype assembly often relies on manual adjustments that cannot
be repeated efficiently at scale. A manufacturer with machining, tooling,
molding, and assembly capability can identify those gaps earlier and recommend
changes before production tooling and inventory commitments are made.
Xiamen Creator Technology
supports this progression by combining product development, custom component
manufacturing, tooling, sourcing, final assembly, and packaging within one
production workflow. The value is not that every product follows the same
route, but that the route can be organized around the product's volume,
complexity, and quality requirements.
Start With a Build Package That Can
Be Executed
The most productive box build projects begin with a
complete, controlled build package. At minimum, this should include a current
bill of materials, assembly drawings or 3D files, approved samples or finish
standards, test requirements, packaging specifications, labeling content, and
revision history. If information is still changing, that is manageable, but the
change process must be clear.
A pilot run is often the right
point to validate the full path: materials receipt, assembly sequence, test
coverage, packaging, and shipment preparation. It exposes issues that a
component-level prototype cannot reveal, including labor bottlenecks, missing
instructions, awkward cable routing, or cartons that do not fit the completed
unit.
The useful question is not
whether a factory can assemble a product once. It is whether the process can
produce the same approved product repeatedly, with known materials, verified
performance, and controlled delivery. That is the standard that turns a
finished design into a dependable production program.