Learn how CNC machining surface finish is controlled by material, toolpaths, cutters, speeds, tolerances, and post-processing for production-ready parts.

A
part can meet every dimensional tolerance on the drawing and still fail at
assembly, sealing, appearance, or customer approval because of its surface. CNC
machining surface finish is not a cosmetic detail added after manufacturing. It
is a controlled result of material behavior, cutting strategy, machine
condition, tooling, and the finish requirement specified on the drawing.
For product teams and sourcing
engineers, the practical question is not simply, “What finish can be achieved?”
It is whether the specified finish supports the part’s function without adding
unnecessary cycle time, secondary processing, inspection burden, or cost.
What CNC Machining Surface Finish
Means
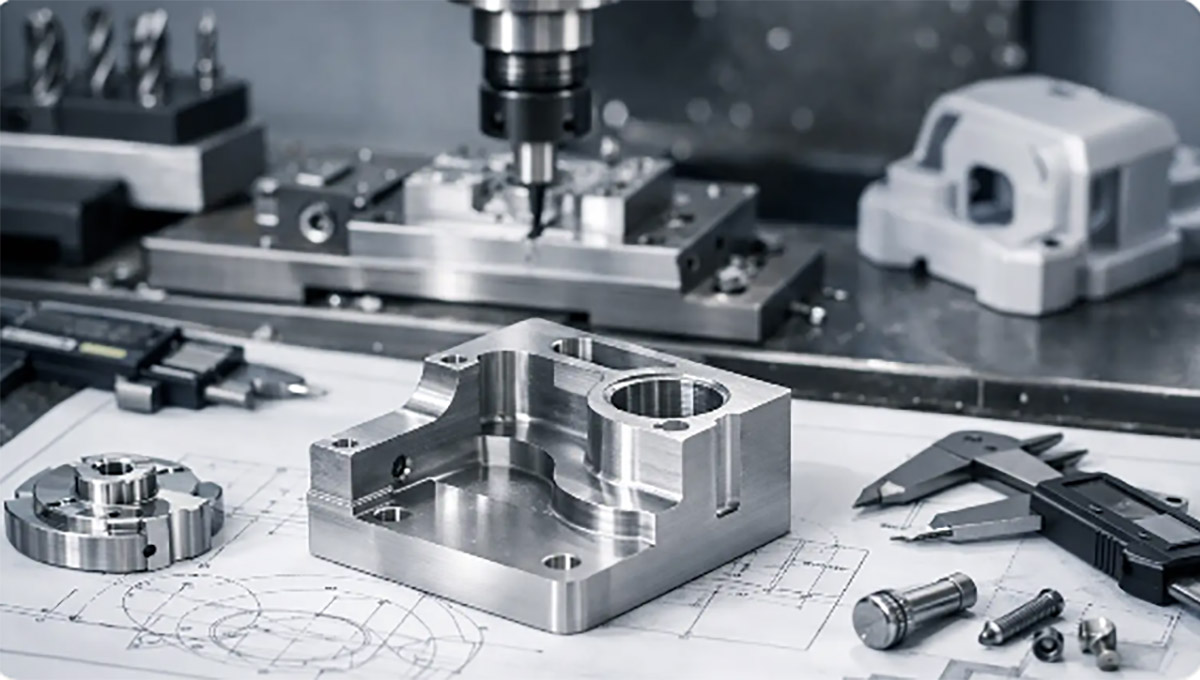
Surface finish describes the texture left on a
machined surface. It is commonly measured as surface roughness, often using Ra,
or arithmetic average roughness. In U.S. manufacturing drawings, Ra is
frequently stated in microinches, although metric values in micrometers are
also common.
A lower Ra value indicates a
smoother surface. For example, a standard CNC-milled face may be suitable around
63 microinches Ra, while a sealing face, sliding interface, or visible consumer
product surface may require 32, 16, or lower. The right target depends on how
the component will perform after machining, coating, molding, assembly, or use.
Ra alone does not tell the
full story. Surface lay, waviness, tool marks, burrs, edge condition, and
localized defects can matter just as much. A circular toolpath pattern may be
acceptable on a recessed pocket but unacceptable on a brushed or polished
visible enclosure. A low roughness reading also does not guarantee a reliable
seal if the face has unevenness or machining marks that run across the sealing
path.
Why Surface Requirements Affect
Cost and Lead Time
Every finish callout should have a functional reason.
Tighter surface requirements can require slower feeds, smaller stepovers,
additional finishing passes, fresh cutters, more rigid fixturing, and closer
inspection. If a part needs polishing, bead blasting, brushing, anodizing,
plating, or painting, surface preparation and handling also become part of the
production plan.
The cost effect is most
noticeable when a low roughness requirement is applied to every surface by
default. Many faces may be hidden inside an assembly or have no contact
function. Applying a fine finish across the full part increases machining time
without improving product performance.
A more efficient drawing
identifies the critical surfaces. For example, a bearing bore, gasket land,
optical interface, cosmetic front face, or mating datum may need a defined
finish. Internal clearance pockets, non-contact walls, and concealed features
can often use the standard as-machined finish. This approach gives the
manufacturing team room to optimize cycle time while protecting the
surfaces that matter.
Surface finish and dimensional
tolerance work together
Fine surface finish cannot compensate for poor
geometry. A polished bore that is out of round, tapered, or incorrectly sized
will still create an assembly issue. Similarly, a flat sealing surface needs
appropriate flatness control, not only a low Ra callout.
Tight tolerances and fine
finishes can also compete with each other. Finishing passes may remove very
small amounts of material, but tool deflection, heat, and clamping stress still
influence final dimensions. The process plan must account for both requirements
from the start rather than treating finish as a last operation.
The Main Factors That Control the
Machined Result
The finished texture comes from the interaction of the
machine, setup, cutting tool, and part material. Good results are repeatable
when these factors are managed as a system.
Material machinability
Aluminum generally machines cleanly and can achieve a
fine finish with proper sharp tooling and chip evacuation. Stainless steel is
tougher and more prone to work hardening, which makes speeds, feeds, and tool
condition more sensitive. Mild steel, brass, copper, titanium, engineering
plastics, and filled plastics each create different surface challenges.
Plastics require particular
care. Excess heat can smear the cut surface, create burrs, or distort thin
features. Softer materials such as silicone cannot be conventionally CNC
machined to the same type of finish as rigid plastics or metals. For molded
components, the tool surface finish also affects the final part appearance and
release behavior.
Tool geometry and tool wear
A sharp, correctly selected cutter is central to a
consistent finish. Tool coating, helix angle, flute count, corner radius, and
tool length all influence chip formation and vibration. A long tool reaching
into a deep cavity may flex, leaving visible chatter even when the programmed
toolpath is correct.
Tool wear often shows up first
as declining surface quality. The part may remain within size tolerance while
showing tearing, discoloration, burrs, or inconsistent machining marks.
Production controls should define practical tool-life limits rather than waiting for
visible failure.
Speeds, feeds, and cutting
engagement
Feed per tooth, spindle speed, radial engagement,
axial depth of cut, and coolant delivery determine how the cutter interacts with
the material. Finishing at an excessively high feed can leave coarse scallops.
Running too slowly can cause rubbing rather than clean cutting, creating heat
and a poor surface.
There is no universal setting
for a “smooth finish.” The correct parameters depend on alloy, part rigidity,
cutter diameter, feature geometry, and machine capability. A proven process
uses appropriate roughing conditions to remove material efficiently, then
leaves controlled stock for a stable finishing pass.
Workholding and machine rigidity
A part that shifts or vibrates during finishing will
show the effect immediately. Thin walls, long unsupported features, and
flexible sheet-like parts are especially sensitive. Fixture design must support
the part without deforming it, while providing tool access to the surfaces that
require finish control.
Machine spindle condition,
axis accuracy, backlash, and vibration also matter. On production parts, a
repeatable fixture and stable machine process are usually more valuable than
chasing a fine finish through manual adjustment on each setup.
Toolpath strategy
The programmed path determines both the surface
pattern and the machining time. For flat faces, a consistent finishing
direction can create a uniform visual appearance. For curved surfaces, smaller
stepovers reduce scallop height but increase cycle time. Ball end mills,
bull-nose cutters, and specialized finishing paths are selected based on the
geometry and finish target.
Entry and exit moves deserve
attention as well. Witness marks at tool transitions can be noticeable on
cosmetic parts and can create functional issues on critical sealing areas. CAM
programming should consider where tool marks will appear, not only whether the
material has been removed.
Selecting an Appropriate Finish Requirement
A practical surface specification starts with the
component’s job. An internal bracket often needs only a standard machined
finish with deburring. A mating aluminum housing may need a controlled finish
on its contact face. A medical, consumer electronics, or display-facing
component may need secondary finishing because the as-machined pattern is
visible and not aligned with the intended product appearance.
Common requirements can be
organized by function:
·
General structural surfaces typically use an as-machined finish with
removed sharp edges and burrs.
·
Mating, sliding, and sealing surfaces require finish values matched to
contact pressure, lubrication, gasket type, and motion.
·
Cosmetic metal parts may require bead blasting, brushing, polishing,
anodizing, or coating after machining.
·
Mold tools often need specific polished, textured, or EDM finishes because
the tool surface transfers to molded parts.
·
Parts receiving paint or plating need a preparation method compatible with
coating adhesion and final appearance.
Avoid specifying a mirror
finish when a controlled machined finish will perform equally well. Polishing
can soften edges, alter small features, round corners, and introduce variation
if it is not carefully controlled. On the other hand, a decorative product
surface may genuinely need polishing or a uniform blast finish to meet brand
standards. The decision depends on function and visual expectations.
Secondary Finishing Processes
CNC machining is frequently one step in the final
finish plan. Bead blasting creates a uniform matte appearance and can reduce
the visual impact of tool marks, but it does not correct dimensional defects.
Brushing produces directional grain for selected cosmetic surfaces. Polishing
can reduce roughness significantly, though it requires attention around edges,
holes, and tight geometry.
For aluminum, anodizing adds
corrosion resistance and can provide clear or colored appearance. The condition
of the machined surface before anodizing remains visible, especially with clear
anodize. For steel components, plating, passivation, painting, powder coating,
or conversion coatings may be selected based on corrosion, wear, conductivity,
and visual requirements.
Secondary operations need to
be planned alongside tolerances. Coating thickness can affect threads, bores,
press fits, and electrical contact points. Masking requirements, racking marks,
and cosmetic acceptance zones should be defined before production rather than
addressed after the first lot is finished.
Inspection and Communication That
Prevent Rework
A reliable surface finish requirement is clear,
measurable, and limited to the areas where it matters. The drawing should
identify the target value, the applicable surface, and any process-specific
appearance requirement. If a surface must be free of tool marks in a particular
direction, that should be stated directly.
Verification may include a
surface roughness tester, visual comparison standards, first-article inspection, and approved cosmetic
samples. For high-volume production, retain an approved master sample or
documented acceptance criteria for color, texture, and machining pattern. This
is particularly useful when parts move through machining, finishing, assembly,
and packaging under one coordinated production plan.
Xiamen Creator Technology
reviews machining, post-processing, and assembly requirements together so
critical surfaces are not treated as isolated drawing notes. That helps
identify finish-related risks before tooling, pilot builds, or volume
production begin.
The most useful next step is
to review each finish callout against the part’s actual function: where it
seals, slides, mates, shows, or receives a coating. That discussion usually
removes unnecessary cost from noncritical faces while giving the critical ones
the process control they need.